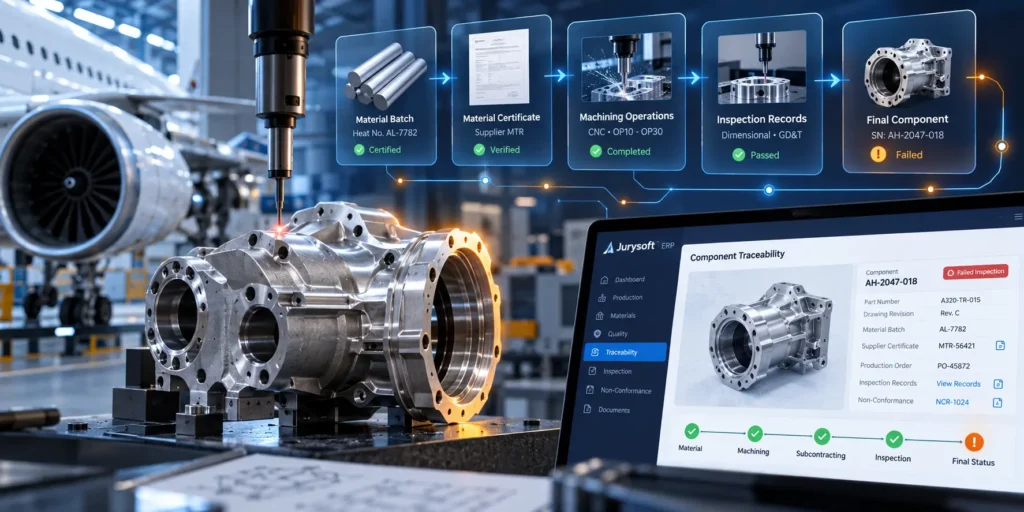
A machined aerospace component has passed through several production stages and reaches final inspection. The quality inspector discovers a dimensional deviation that exceeds the tolerance specified on the approved engineering drawing.
The component is placed on hold. Before deciding whether it can be reworked, repaired, or rejected, the quality team must establish exactly what happened during its manufacture.
The investigation begins with several questions:
- Which raw material batch was used to manufacture the component?
- Where is the original material test report or supplier certificate?
- Which machining operations were performed, and by whom?
- Were the correct drawing revision and GD&T requirements followed?
- What were the results of previous in-process and final inspections?
- Were other components manufactured from the same material batch?
These questions are difficult to answer when material certificates are stored in shared folders, production details are recorded on paper job cards, and inspection results are maintained in separate spreadsheets.
For aerospace manufacturers, traceability must connect the physical component to its material origin, production history, inspection evidence, and quality decisions.
Aerospace component traceability software helps establish these connections by maintaining a structured record of component genealogy throughout the manufacturing process. When integrated into an aerospace manufacturing ERP system, it can make investigations faster, more consistent, and easier to document.
1. Why Component Traceability Breaks Down in Aerospace Manufacturing
Aerospace components often pass through multiple stages, including raw material receiving, cutting, machining, heat treatment, surface finishing, inspection, and final release. Some operations may also involve approved external processors.
Every stage can create records that must remain connected to the correct component or material batch.
Missing material batch references
A manufacturer receives an aluminium alloy bar with a supplier batch number and an accompanying material test report. The receiving team records the batch in the inventory system.
Later, an operator issues part of the bar to a production order. If the material issue transaction does not preserve the original batch reference, the finished components may no longer be reliably linked to that source material.
Disconnected material certificates
Supplier certificates may be saved as PDF files using inconsistent names. The purchasing team knows the supplier, the warehouse knows the receipt number, and quality knows the material specification, but nobody can immediately identify the certificate associated with a particular component.
Material certification tracking should link each certificate to the relevant supplier, receipt, material specification, and batch or lot.
Incomplete machining records
A paper job card might identify a production order but omit the component serial number, operation revision, machine identifier, or inspection result.
If a defect appears later, the manufacturer may struggle to establish which components passed through the affected operation under the same conditions.
Gaps in subcontractor records
Heat treatment, plating, coating, or other special processes may be performed externally. If dispatch records, processor certifications, batch references, and return inspections are not linked to the original production order, the component’s history becomes fragmented.
The problem is not simply a lack of documents. It is the loss of reliable relationships between those documents and the component being investigated.
2. Connecting Incoming Material Certificates to Production Orders
Traceability begins when raw material enters the facility, not when a finished component fails inspection.
An aerospace manufacturing ERP system should establish a traceable relationship between incoming material, supplier documentation, receiving inspection, inventory, and production consumption.
Step 1: Record the material identity
When material arrives, record the relevant details, such as:
- Material grade and specification
- Supplier and purchase order
- Supplier batch, heat, or lot number, as applicable
- Internal receipt or inventory lot number
- Quantity received and storage location
- Material test report or certificate reference
- Receiving inspection result and release status
The system should preserve the original supplier identifiers alongside internal tracking references. An internal lot number must not silently replace or obscure the supplier’s original batch identity.
Step 2: Link the certificate to the material batch
The certificate should be linked directly to the relevant receipt and material lot, with controls that help prevent an incorrect or unverified document from being associated with the batch.
Depending on the material and customer requirements, the record may include chemical composition, mechanical properties, specification compliance, and other supporting information.
Quality personnel should be able to retrieve the applicable certificate from the material record without searching unrelated folders.
Step 3: Control material release
Material should only become available for production when the required receiving checks and approvals are complete.
For example, if an aluminium alloy batch is awaiting certificate verification, the inventory record should show that status and prevent unauthorised issue to a production order.
The precise hold and release rules should follow the manufacturer’s approved quality procedures and applicable customer requirements.
Step 4: Record every material issue
When the material is issued to a work order, the transaction should capture the source lot, quantity consumed, production order, and relevant component or serial references.
If one source batch supplies multiple production orders, the ERP should preserve each consumption relationship. If one component incorporates multiple traceable material lots, the system should support that relationship where the manufacturing process and applicable requirements demand it.
This creates the foundation for tracing a finished component backward to its material origin and tracing a suspect batch forward to potentially affected production.
3. Maintaining Traceability Through Machining and Subcontracting
Material genealogy alone is insufficient. The manufacturer also needs to know what happened to the material after it entered production.
Maintain operation-level production history
Consider a machined aerospace housing manufactured through the following routing:
- Raw material cutting
- CNC rough machining
- CNC finish machining
- Dimensional inspection
- Approved surface treatment
- Final inspection
Each operation should be linked to the relevant work order and component or lot identity.
Depending on the manufacturer’s process, useful records may include the operation completion date, operator identification, machine or equipment reference, approved program or process revision, measured values, inspection status, and any authorised deviation.
These records help investigators narrow down where a defect may have originated. They do not, by themselves, prove the root cause.
Preserve traceability during material transfers
When material moves from a central store to a production area, or when work in progress moves between operations, the traceability reference should remain intact.
Splitting a batch into several jobs, combining permitted material quantities, or generating new internal identifiers must follow defined genealogy rules. The original source relationships should remain retrievable.
Track external processing
When components are sent to an outside processor, record the relevant dispatch, processor, quantity, component identities, applicable process requirements, and return documentation.
After the components return, link the processing certificate or report to the correct components or lots. Record incoming verification and any quality hold or rejection.
For special processes, supplier approval and evidence requirements should be defined by the applicable aerospace quality system, contract, and customer requirements.
An ERP system should not treat a completed subcontracting purchase order as proof that the external process was acceptable. The required documentation and verification must be completed before the components progress to the next controlled stage.
4. Investigating a Failed Inspection Using Component Genealogy
The real value of aerospace component traceability software becomes clear when a non-conformance is discovered.
Imagine that component serial number AH-2047-018 fails final dimensional inspection. A critical bore measures outside the permitted tolerance specified on the approved drawing.
The quality team opens a non-conformance record and places the affected component on hold.
A structured investigation follows.
Step 1: Start with the component serial number
The serial number should lead to the relevant production order, part number, drawing revision, routing, and recorded inspection results.
This establishes which requirements applied to the component and which manufacturing steps were completed.
Step 2: Identify the original material batch
The material-consumption record links the component or production order to the source inventory lot.
The quality team can then retrieve the supplier’s batch or heat identification, receiving record, material specification, and associated certificate.
If the material was cut into several blanks or allocated across different orders, the genealogy records should show those relationships.
Step 3: Review machining and process history
The investigator examines the routing and operation records to identify the machining stages completed before the failure.
Relevant evidence may include CNC operation records, tooling or equipment references, approved program revisions, recorded process parameters where required, and operator sign-offs.
If the component passed an earlier inspection, that result can be compared with the failed final measurement. This helps establish when the deviation was first detected, although further technical analysis may be needed to determine why it occurred.
Step 4: Retrieve inspection evidence
The ERP should connect the component to its inspection plan, applicable drawing revision, acceptance criteria, measured values, inspector records, and final disposition.
For a GD&T-controlled feature, the inspection record should identify the characteristic being measured and the applicable tolerance requirements. Where relevant, it should also reference the approved measurement method and equipment.
A simple status marked “Passed” may not provide sufficient evidence for a detailed investigation. The required level of recorded measurement data depends on the inspection plan, contractual obligations, and the manufacturer’s quality procedures.
Step 5: Record the non-conformance and investigation
The investigation record should capture the detected deviation, containment actions, supporting evidence, investigation findings, corrective actions where applicable, and authorised disposition.
Possible dispositions may include rework, repair under an approved process, use-as-is under the required authorisation, or rejection. The appropriate decision depends on the applicable technical, regulatory, contractual, and customer requirements.
Important: Traceability software supports the investigation and documentation process. It does not automatically determine whether a component is airworthy, acceptable for use, or eligible for a particular disposition.
5. Identifying Other Components That May Be Affected
Investigating the failed component is only one part of the response. The manufacturer must also determine whether other components could share the same risk.
Suppose the investigation identifies a potential issue associated with material batch AL-7782.
A traceability-enabled ERP should help the quality team identify:
- Other production orders that consumed material from batch AL-7782
- Components manufactured from the affected source material
- Work in progress that may require a hold
- Finished components awaiting inspection or release
- Shipped components that may require further assessment under established escalation procedures
The resulting list is an investigation starting point, not an automatic declaration that every related component is defective.
Quality and engineering teams must evaluate the evidence, define the relevant scope, and decide on containment and any customer or regulatory communication required by applicable procedures.
The same logic can be applied in the opposite direction. If an investigation points to a particular machining operation, equipment condition, or subcontracted process, the team can search for other components that passed through the potentially affected process during the relevant period.
This combination of backward and forward traceability helps manufacturers establish the scope of a quality issue more systematically.
6. What an Aerospace ERP Traceability Record Should Contain
The precise data requirements vary by component, customer, contract, and quality system. However, a useful traceability record should connect the following information.
| Record area | Information to maintain |
|---|---|
| Component identity | Part number, serial or lot number, and production order |
| Engineering control | Approved drawing revision, applicable specifications, and authorised changes |
| Material origin | Supplier, material specification, original batch or heat number, and internal lot |
| Material certification | Certificate reference, linked document, verification status, and approval history |
| Production history | Routing, operation completion, relevant equipment references, and process records |
| Subcontracting | Processor identity, dispatch and receipt references, certificates, and verification |
| Inspection | Inspection plan, characteristic, applicable tolerance, results, inspector, and status |
| Non-conformance | Defect description, containment, investigation, corrective action, and disposition |
| Audit history | User actions, timestamps, approvals, and controlled record changes |
The system should also support role-based access, controlled revisions, reliable document retrieval, and protection against unauthorised changes.
Where records are corrected, the system should preserve the required history instead of silently overwriting previous values. Electronic approvals and records should be managed according to applicable customer, contractual, regulatory, and quality-system requirements.
7. How AS9100, NADCAP, and GD&T Fit Into the Traceability Workflow
Traceability must support the manufacturer’s actual quality obligations rather than relying on a generic software checklist.
AS9100 Rev D
AS9100 Rev D includes requirements related to operational control, identification and traceability, control of externally provided processes, production controls, monitoring and measurement, and the control of non-conforming outputs.
An ERP system can help implement these controls by linking material records, production operations, inspection evidence, and quality approvals.
However, using ERP software does not by itself establish AS9100 conformity or guarantee certification. The organisation must implement and maintain the applicable processes and demonstrate their effectiveness.
NADCAP special-process controls
NADCAP accreditation is relevant to specific aerospace special processes and participating supply-chain requirements. Where a component undergoes a covered process, manufacturers may need to maintain evidence relating to the approved processor, applicable process, processing records, certification, and acceptance checks.
The ERP should link these records to the correct component or material batch. It should also support checks that reflect the manufacturer’s approved supplier and process-control procedures.
Not every aerospace manufacturer or component requires every NADCAP accreditation. Applicability depends on the process, customer, contract, and supply-chain requirements.
GD&T and inspection evidence
Geometric Dimensioning and Tolerancing defines how engineering requirements for part geometry are communicated and evaluated.
For example, a bore may satisfy its nominal diameter requirement but fail a positional tolerance relative to a specified datum reference frame.
The inspection record should therefore identify the relevant characteristic and applicable drawing revision, along with the measurement result and required supporting evidence.
An ERP system can connect this evidence to the component’s manufacturing history and non-conformance record. It should not replace the engineering drawing, approved inspection method, or competent quality and metrology personnel.
8. How to Test Traceability Before an Aerospace Quality Audit
A manufacturer should not assume traceability is effective simply because material batches and certificates exist in the ERP.
Run a mock investigation using a randomly selected finished component or an appropriately selected sample from the quality team.
Start with the component’s serial or lot number and attempt to retrieve the required production and quality records without relying on undocumented knowledge held by individual employees.
Then run a forward-traceability exercise using a selected material batch to identify the production orders and components associated with it.
Measure:
- Time required to identify the original material batch
- Time required to retrieve the applicable supplier certificate
- Completeness of the component’s production and inspection history
- Accuracy of the list of potentially affected components
- Number of missing, inconsistent, or manually reconstructed records
- Time required to produce an investigation evidence package
For example, a manufacturer might discover that retrieving a material certificate takes 25 minutes because staff must search several folders and verify the batch manually. After implementing linked material records and validated document references, the same retrieval might take three minutes.
These are illustrative figures, not guaranteed savings or measured results from Jurysoft customers. Actual performance should be established through a documented before-and-after test.
The objective is not merely faster retrieval. The investigation must also be complete, accurate, controlled, and reproducible.
9. Aerospace Manufacturing ERP Implementation Checklist
Before implementing or improving aerospace component traceability software, review the following controls.
- Define which parts, materials, operations, and products require batch or serial-level traceability.
- Preserve supplier batch, heat, and lot identifiers alongside internal inventory references.
- Link material certificates and supporting documents to the correct receipts and inventory lots.
- Configure receiving inspection, quarantine, release, and material-issue controls.
- Connect material consumption to the appropriate production order and component genealogy.
- Maintain controlled drawing revisions, routings, and authorised engineering changes.
- Capture the operation and inspection records required by the approved manufacturing process.
- Link subcontractor processing records and certificates to the relevant components or lots.
- Connect non-conformance records to affected components, investigation evidence, and authorised dispositions.
- Test backward traceability from a finished component to its source material.
- Test forward traceability from a material batch to potentially affected components.
- Establish role-based access, audit history, record retention, and approval controls.
- Run mock investigations and document retrieval-time and record-completeness results.
Prioritise the controls that address actual gaps in your workflows. An implementation should reflect the manufacturer’s product complexity, traceability obligations, existing systems, and customer requirements.
Conclusion: Make Every Aerospace Component’s History Retrievable
When an aerospace component fails inspection, the manufacturer needs more than an inventory balance or a folder of certificates. The quality team needs a connected history that establishes where the material came from, how the component was manufactured, which inspections were performed, and what decisions were made.
Aerospace component traceability software can help connect these records across receiving, production, subcontracting, inspection, and non-conformance management.
The result is a more structured approach to quality investigations, material containment, audit preparation, and the identification of potentially affected components.
For aerospace manufacturers, the key question is straightforward: Can your team trace a failed component back to its original material batch and retrieve the supporting records without reconstructing its history manually?
If the answer is uncertain, it may be time to assess the gaps in your current manufacturing systems.
Request a Free ERP Gap Audit from Jurysoft
Jurysoft helps manufacturers evaluate their ERP workflows, operational visibility, and system integration requirements.
A review of your current processes can help identify gaps in material batch traceability, certificate management, production history, inspection records, and non-conformance workflows.
Request your Free ERP Gap Audit: https://jurysoft.com/erp/free-erp-gap-audit/
Identify where your traceability process needs improvement and establish a practical path toward more connected manufacturing and quality records.